

Decoding Quality: Choosing the Right Light Graphite Color
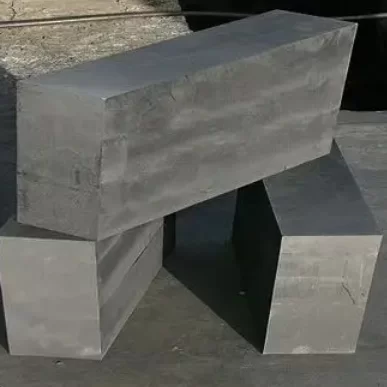
In the metallurgy and material science industries, visual inspection is often the first line of defense against inefficiency. Procurement managers frequently struggle with inconsistency in raw materials, where a dull, dark finish often signals incomplete graphitization or high impurities. Identifying a distinct, metallic light graphite color is not merely an aesthetic preference; it is a critical indicator of crystalline alignment and electrical performance. When the color is off, the conductivity drops, and production costs rise.
Ding An Heng New Material Technology Co., Ltd. addresses this challenge by controlling the entire production lifecycle, from calcining to the final graphitization. With over 20 years of benchmarking experience and a facility covering 88,000 square meters, we ensure that every product exhibits the signature lustrous light graphite color that signifies high purity and low electrical resistance. Our 60,000-ton annual capacity is managed under strict ISO and SGS certified protocols, guaranteeing that the visual promise of our materials is matched by their structural integrity in your furnaces.
Engineering Standards Behind the Light Graphite Color
The specific shade of graphite—specifically a silvery light graphite color—is a direct result of high-temperature treatment exceeding 2,500°C, which removes volatile impurities and aligns carbon atoms into a hexagonal lattice structure. Dull materials often indicate high ash content or insufficient heat treatment. At our standardized labs, we correlate this visual attribute with quantifiable metrics such as specific electrical resistance and flexural strength.
By leveraging two complete sets of production lines covering impregnation and secondary baking, we achieve a degree of graphitization that results in the optimal hue and performance. The table below outlines how the light graphite color correlates with our engineering standards compared to general market averages.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Graphitization Degree | Determines the "Lightness" of the color and conductivity. | > 98% (Premium Grade) | Achieves the distinct light graphite color indicating maximum conductivity. |
| Ash Content | Impurity levels that darken the material. | Minimized (High Purity) | Prevents slag contamination in steelmaking. |
| Resistivity | Inverse to color brightness; lighter = lower resistance. | Optimized for UHP/HP Grades | Reduces energy consumption significantly. |
| Visual Consistency | Indicator of batch uniformity. | 100% Uniform Luster | Ensures stable performance across large shipments. |
Maximizing ROI with Consistent Light Graphite Color
Global markets, ranging from the Middle East to Russia, rely on suppliers who can deliver consistency. Sourcing materials with a verified light graphite color serves as a proxy for value engineering; it ensures that the graphite electrodes or additives will perform predictably under high thermal stress. Investing in high-grade, light-colored graphite reduces electrode consumption per ton of steel, directly impacting the operational bottom line.
With total assets of 600 million and a track record of exporting to over 250 countries, we provide the supply chain stability required for long-term planning. The chart below illustrates the correlation between the intensity of the light graphite color (represented by Graphitization Degree) and the reduction in Electrical Resistivity, demonstrating the clear financial advantage of choosing high-purity materials.
Related products


Top Selling Products



How to Choose Polish Varnish Cleaner & Graphite Compound Tools for Your Process

Factors Affecting the Spherical Graphite Price and Market Trends

Industrial Analysis of the Price of Graphite per Pound


